Description
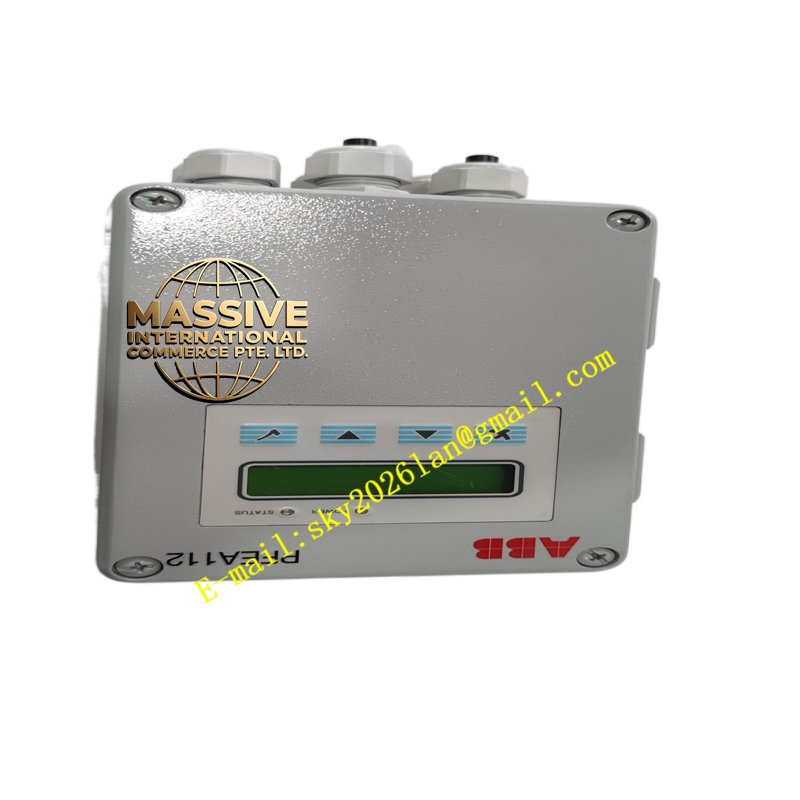
ABB PFEA112-65 3BSE050091R65
Technical Specifications:
- System Composition: Operates as the central electronic processing unit paired with two mechanical press heads.
- Measurement Units: Supports multiple selectable tension units including N, kN, MN, kp, t, lb, and T.
- Communication Interface: Equipped with a Profibus-DP interface for seamless integration into higher-level automation systems.
- Input/Output: Features easily configurable analog and digital input/output ports.
- Measurement Range: Default measurement range is typically 10 times the Nominal Load (Fnom), but can be customized for higher precision.
Functional Features:
- Closed-Loop Control: Converts mechanical pressure into tension data and transmits it to the automation system to form a precise closed-loop tension control.
- Advanced Configuration: Includes a step-by-step menu for setting up the control unit, threshold judgment, and simulation functions to easily verify system integration.
- Comprehensive Diagnostics: Features a built-in self-diagnostic testing system that includes continuous sensor testing for reliable operation.
- Remote Management: Supports network connectivity for remote access and allows parameter import/export via a PC for streamlined maintenance.
Application Scenarios:
- Continuous acid rolling and cold rolling production lines.
- Web handling systems in steel, aluminum, and paper manufacturing.
- Applications where precise tension control is critical to preventing thickness deviations or strip breakage.
Performance Parameters:
- High Precision: Delivers exceptional measurement accuracy, which directly dictates the precision of the production line’s tension control.
- Load Division Resolution: Automatically calculates the Load Division based on the configured measurement range (e.g., a 50kN unit can achieve a 40N resolution when configured to a 200kN range).
- Zeroing Capability: Provides a dedicated SetZero function for accurate baseline calibration before threading the strip.
Material Composition & Structural Characteristics:
- Electronic Housing: Robust industrial enclosure housing the control unit, isolation amplifiers, and terminal boxes.
- Internal Circuitry: High-precision analog-to-digital converters and signal conditioning circuits designed to process micro-volt signals from piezomagnetic sensors.
- User Interface: Integrated front panel with buttons for local menu navigation and parameter adjustment.
Working Principle:
The unit receives analog pressure signals from two piezomagnetic load cells installed on a guide roll. When the strip passes over the roll at a specific wrap angle, the tension generates force components. The PFEA112 processes these signals, applies the configured Wrap Gain (based on the wrap angle), compensates for tare weight (roll and bearing weight), and calculates the absolute tension. The final value is transmitted via Profibus to the PLC for real-time actuator adjustment.
Installation Requirements:
- Parameter Setup: The Nominal Load must be set strictly according to the rating printed on the load cell’s nameplate.
- Wrap Angle Calibration: The Wrap Gain parameter must be accurately calculated and set based on the actual wrap angle of the strip over the measurement roll.
- Communication Setup: Profibus communication must be enabled in the Miscellaneous Menu, and the correct node address must be assigned.
- Pre-Operation: Always perform a SetZero operation before threading the material to ensure accurate baseline measurement.
Usage Precautions:
- Range Optimization: Avoid using the default maximum measurement range if the actual process tension is much lower. Reducing the measurement range significantly improves the resolution and accuracy of the tension reading.
- Sensor Handling: The connected load cells rely on delicate piezomagnetic principles; avoid excessive mechanical shock during installation.
- Parameter Integrity: Use the PC import/export function to back up configuration parameters before performing major maintenance or firmware updates.