



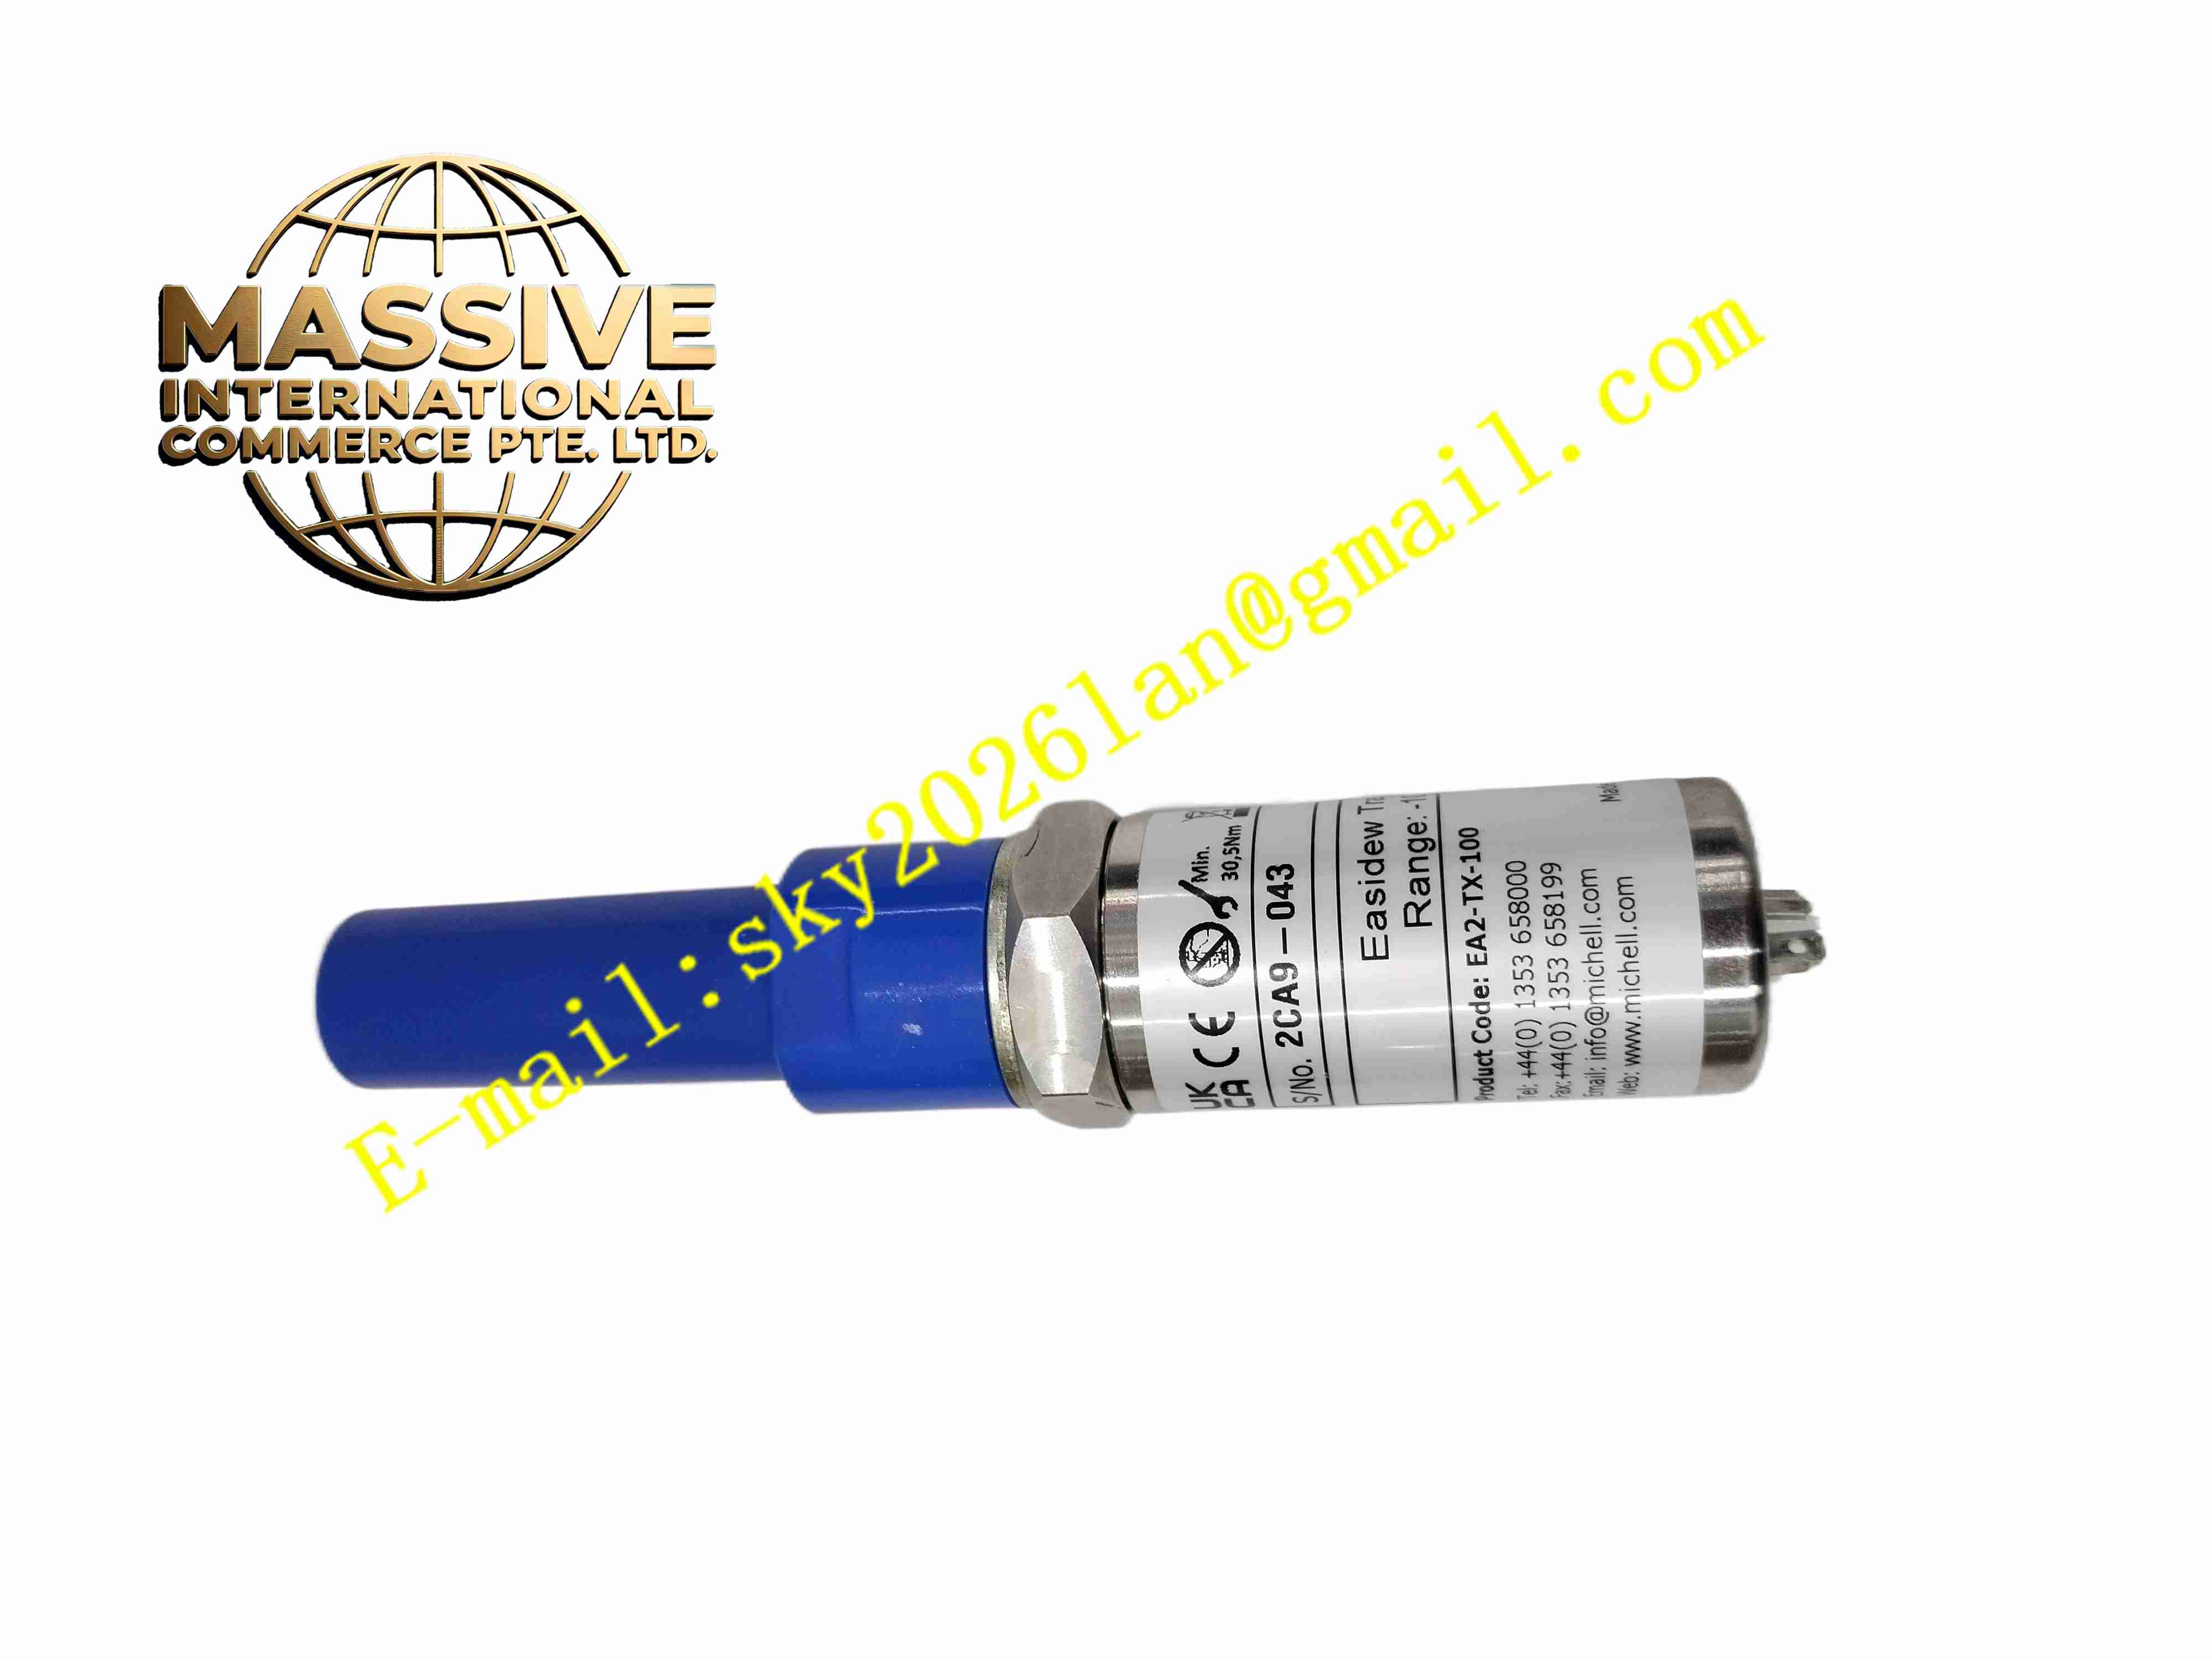
Description
Michell EA2-TX-100
Technical Specifications:
- Measurement Range: -100°Cdp to +20°Cdp
- Measurement Accuracy: ±2°C dew point
- Output Signal: 4-20mA 2-wire loop powered
- Supply Voltage: 12V DC to 28V DC
- Maximum Working Pressure: 450 bar
- Response Time T95: 5 minutes from dry to wet condition
- Repeatability: ±0.5°C dew point
- Process Connection: 5/8″ UNF thread
- Housing Material: 316 stainless steel
- Protection Class: IP66
- Operating Temperature: -40°C to +60°C
Function Features:
- 2-wire loop power design reduces field wiring cost
- Ceramic moisture sensor with long-term stability
- Fully factory calibrated with traceable calibration certificate
- Output configurable for dew point or ppmV moisture content
- Built-in overpressure protection
- Sensor contamination resistance for compressed air applications
- No local display option, transmits measurement via 4-20mA
- Compact probe design for direct insertion into gas pipeline
Application Scenarios:
- Compressed air dryers moisture monitoring
- Instrument air quality measurement
- Natural gas and process gas moisture detection
- Pharmaceutical and food process dry gas monitoring
- Industrial gas generation plants
Material Composition:
- Probe Body: 316 stainless steel
- Sensor Element: Michell ceramic moisture sensor
- Internal PCB: FR4 fiberglass circuit board with microprocessor and signal conditioning chips
- Connector: Plastic DIN 43650 field connector
- Seals: PTFE and FKM sealing gaskets
Structural Features:
- Cylindrical stainless steel probe assembly
- Threaded process fitting for pipeline mounting
- Ceramic sensor tip at probe end exposed to process gas
- Rear DIN connector for 2-wire signal and power connection
- IP66 sealed housing for field installation
Working Principle: The ceramic moisture sensor absorbs water vapor from process gas. The sensor impedance changes proportionally with moisture concentration, which relates directly to dew point temperature. Onboard microprocessor converts sensor impedance signal into dew point value and drives 4-20mA loop current output. The 2-wire loop carries both power supply and measurement signal back to control system.
Installation Requirements:
- Install probe into gas pipeline or sample chamber via 5/8″ UNF thread
- Orient probe to avoid liquid condensate contacting sensor tip
- Use proper sealing gasket to prevent gas leakage
- Run shielded twisted pair cable for 4-20mA loop wiring
- Keep transmitter away from high temperature heat sources
- Avoid mechanical shock to the ceramic sensor tip
Usage Notes:
- Prevent liquid water impinging directly on sensor element
- Verify loop resistance and power supply voltage during commissioning
- Do not expose sensor to corrosive gas outside rated specification
- Perform periodic calibration per site maintenance schedule
- Disconnect loop power before removing transmitter from process line
- Handle probe carefully to avoid damaging ceramic sensor tip







