



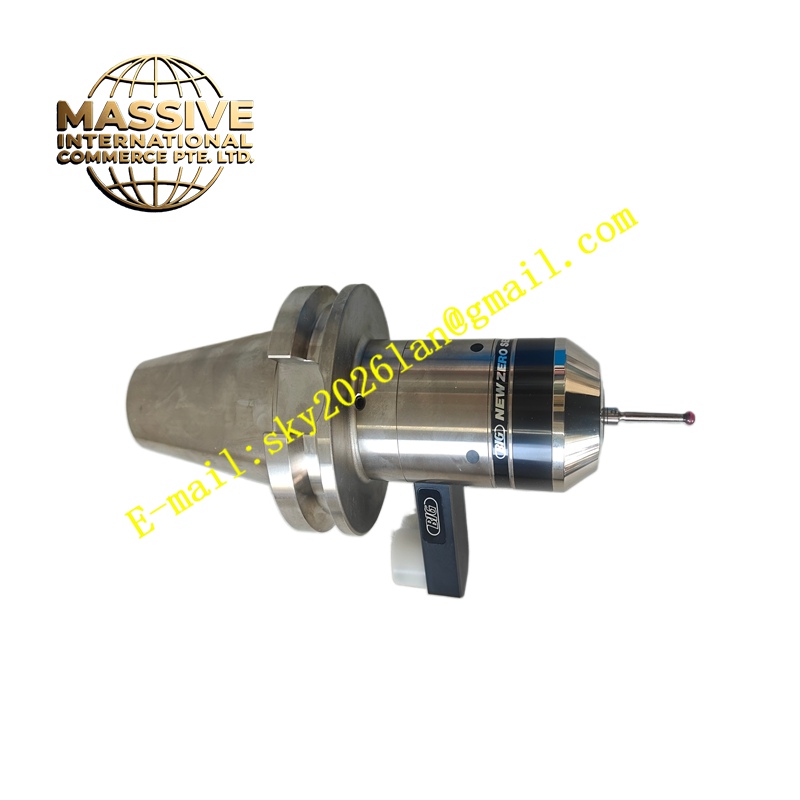
Description
Big Daishowa BT50-LCZ56T-195
Technical Specifications BT50 taper shank conforming to Japanese BT standard; LCZ precision boring head mounting interface; projection length 195mm; maximum compatible boring head diameter 56mm; material alloy steel; surface hardness HRC 58 to 62; dynamic balance grade G2.5 at specified spindle speed; coolant through center capability.
Functional Features Mate with BT50 machine spindle taper for precise radial and axial positioning. Clamp LCZ series fine boring heads securely and transmit spindle torque to cutting tools. Deliver internal coolant through the center bore of the tool holder to the cutting edge for chip evacuation and cutting temperature reduction. Maintain high rotational concentricity during high-speed spindle operation. Allow fast exchange of boring heads for different machining diameter requirements.
Application Scenarios CNC machining center precision boring, mold manufacturing fine finishing, automotive component precision machining, hydraulic valve block bore finishing, heavy-duty milling and boring processes.
Performance Parameters Low runout error at tool mounting face; high rigidity under heavy cutting load; stable dynamic balance at high spindle speed; consistent taper contact precision after repeated tool change cycles.
Material Composition Main body is high-alloy tool steel; taper surface and tool mounting locating surface receive quenching and tempering heat treatment; surface adopts anti-rust black oxide coating; internal coolant passage polished to reduce coolant flow resistance; clamping screw material is high-strength alloy steel.
Structural Characteristics Tapered BT50 shank with pull stud mounting thread at the rear end. Front end features LCZ standard precision boring head locating flange and clamping thread. A central through bore runs the full length for coolant delivery. External cylindrical surfaces are precision ground for minimal rotational runout.
Working Principle The machine spindle drawbar pulls the BT taper shank inward to establish rigid contact between taper surfaces, ensuring coaxial alignment between spindle and tool holder. Spindle rotation transmits through friction contact of the taper. The front flange and clamping mechanism lock the LCZ boring head so the boring head rotates synchronously with the spindle. Coolant pumped through the spindle flows through the central bore of the tool holder to reach the cutting edge.
Installation Requirements Install the compatible pull stud onto the rear thread of the tool holder with specified torque. Mount the LCZ boring head onto the front locating flange and tighten the clamping screw according to torque specification. Clean spindle taper surface and tool holder taper surface thoroughly to remove chips and contaminants. Load the tool holder into the CNC spindle and perform runout inspection before cutting operation.
Precautions for Use Avoid collision of the taper shank and locating flange with hard workpieces or fixtures. Do not exceed the maximum rated spindle speed defined for the balance grade. Apply anti-seize lubricant on pull stud threads as recommended. Inspect taper surface for scratches and wear periodically.







